Sheet lasers get the attention, but tube is where fabrication labor hides. A frame that needs forty tubes traditionally needs forty saw cuts, a marking-out session, dozens of drilled holes, milled notches, and a fitter persuading it all square before welding. A tube laser collapses that chain into programs and chucks. This guide explains how the machines work, which chuck configuration and capacity to buy, the joinery features that justify the investment, and the labor arithmetic behind the category's growth.
Why Tube Cutting Is Its Own Machine
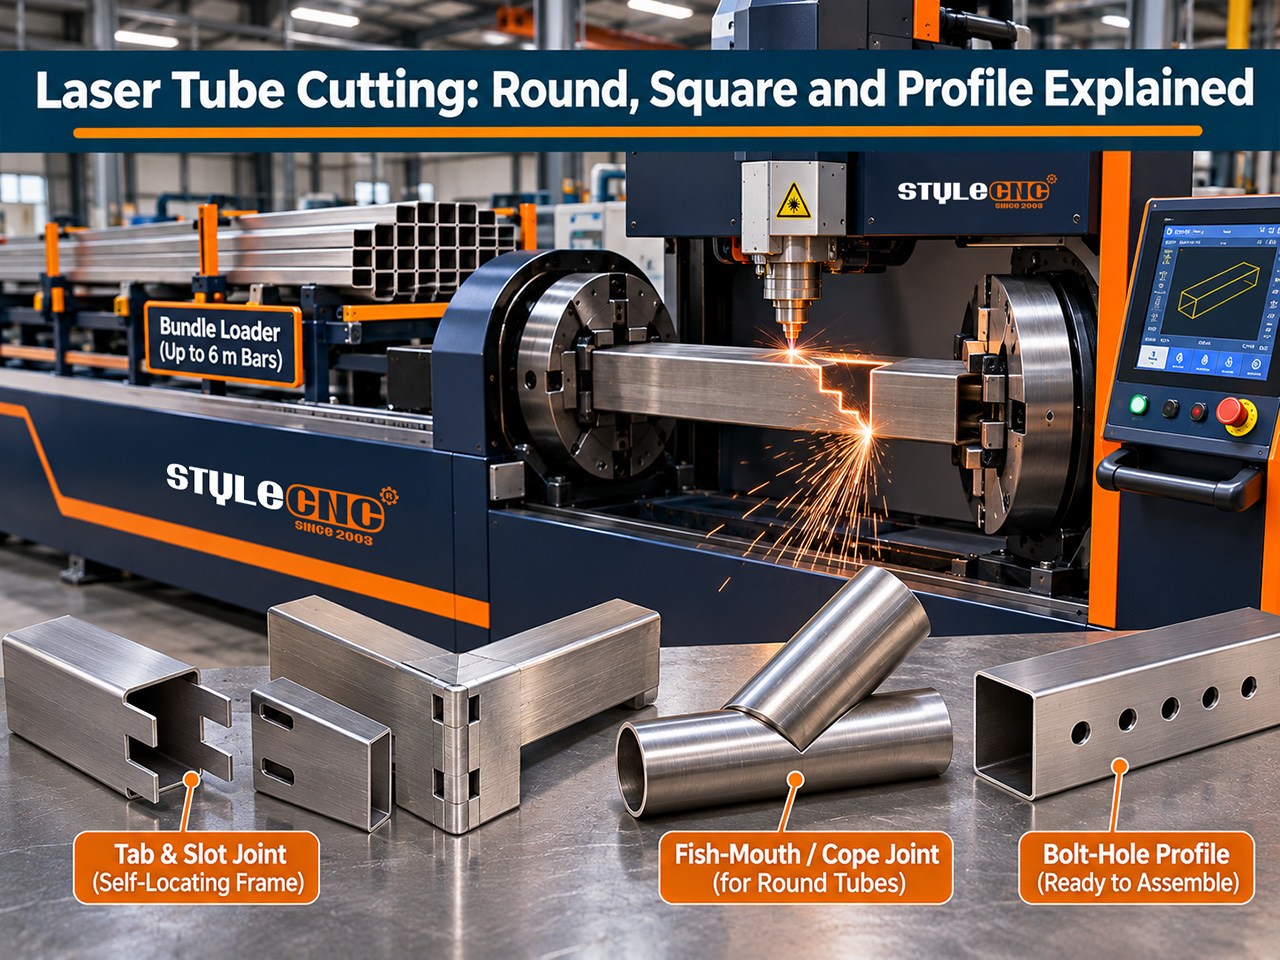
A tube laser is not a sheet machine with a rotary bolted on. The material is a long, heavy bar that must rotate precisely while being fed axially, so the architecture is built around chucks: motorized jaws that grip, spin, and advance the stock through a fixed cutting zone. The controller synchronizes rotation, feed, and the cutting head so a contour can wrap around a corner of square tube or spiral along a round one.
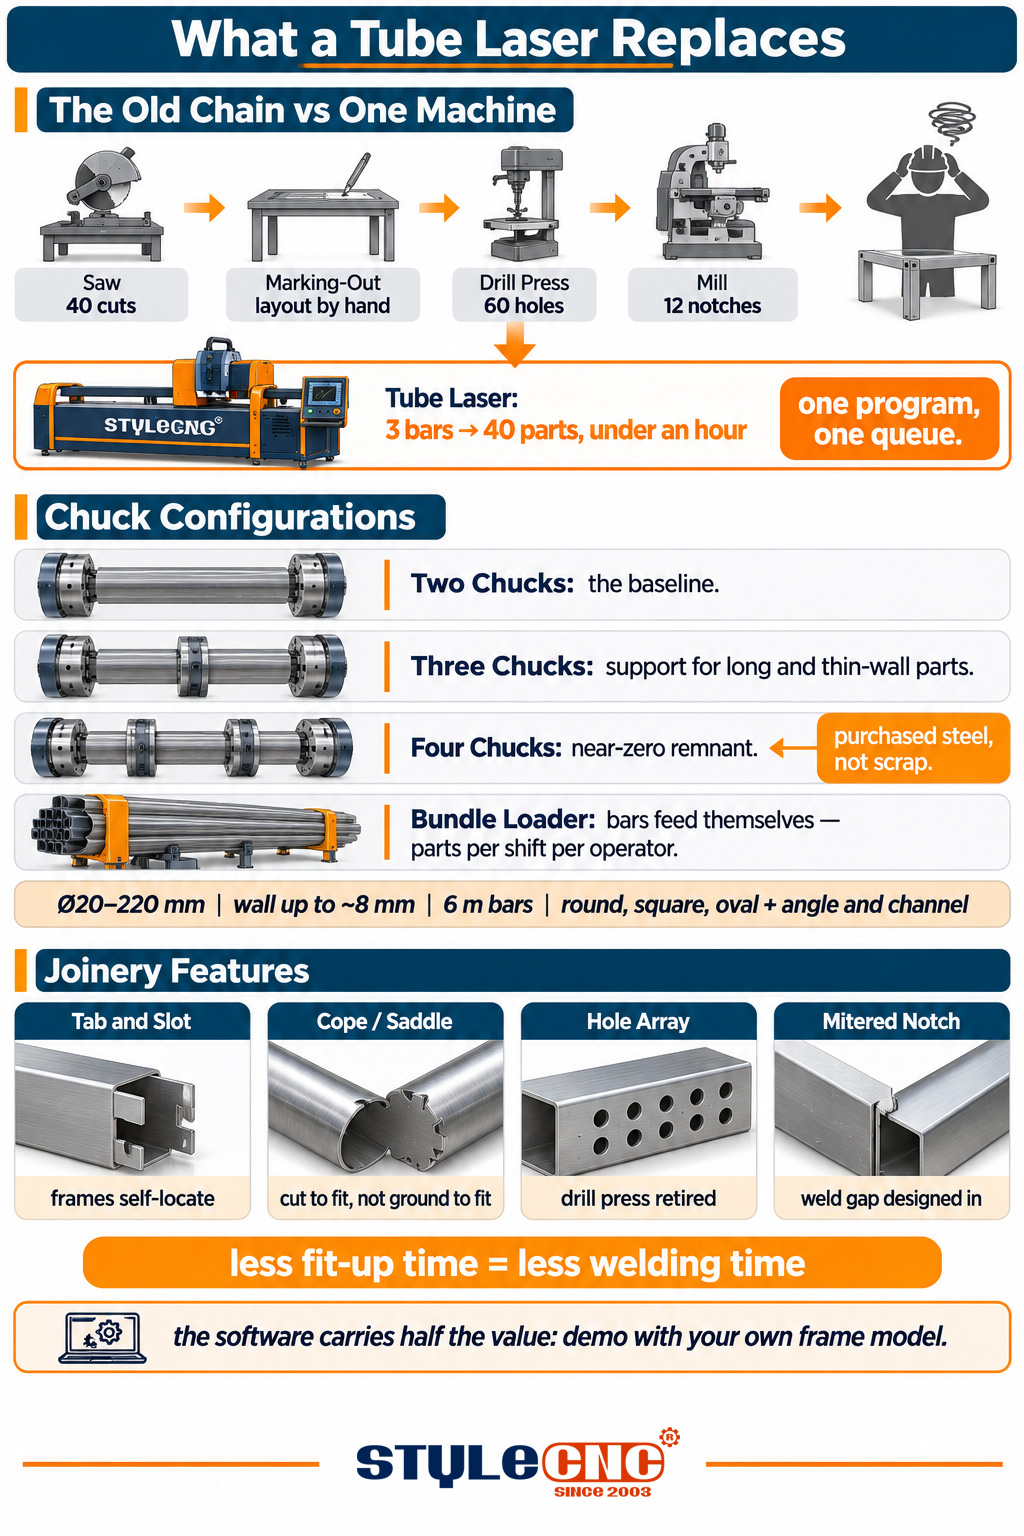
Support is the quiet engineering problem. A 6-meter bar whips and sags if gripped only at its ends, and wall thickness as light as fencing tube dents under careless clamping, which is why chuck count and support design separate the machine classes:
| Конфигурация | Что это добавляет | Для каких задач | Измерения |
|---|---|---|---|
| 2 патронов | The baseline: front chuck feeds and rotates, rear chuck grips the stock | General fabrication on common tube sizes and lengths | Shortest remnant the machine leaves per bar |
| 3 патронов | A middle chuck supports the tube through the cutting zone | Longer parts, thin walls, and tighter remnant control | Vibration and cut quality near bar ends |
| 4 патронов | Full support along the bar with near-zero remnant designs | Production shops where material yield is money | Usable length cut from each purchased bar |
| Auto loading bundle | A rack feeds bars in and parts drop out without an operator at the chuck | Lights-out and high-volume production | Parts per shift per operator |
Remnant length deserves the attention the table gives it. Every bar ends with a stub the chucks cannot feed past, and across thousands of bars that stub is purchased steel in the scrap bin. Designs that cut the remnant to a few centimeters, or near zero on 4-chuck machines, quietly repay their premium in material yield.
Capacity: Diameter, Wall, and Length
⦿ Diameter range: mainstream machines cover roughly 20 to 220 mm across round, square, rectangular, and oval sections; heavy models extend well beyond for structural work.
⦿ Wall thickness: up to about 8 mm on typical configurations, set by laser power; thicker walls call for higher wattage.
⦿ Stock length: standard machines load 6 m bars, with longer-bed options; part length is limited by the machine's unload side.
⦿ Profiles beyond tube: many machines also cut angle, channel, and flat bar, which widens the work a single machine can quote.
Match capacity to the catalog, not the brochure: the machine must swallow your largest regular section with clamping room to spare, and laser power must carry your thickest wall at production speed. The wattage-to-thickness relationship is the same one documented in the fiber laser cutting thickness, speed, and power guide, applied to wall thickness instead of plate.
Thin walls and cosmetic sections
2 capacity details separate adequate machines from frustrating ones. Thin-wall tube, common in furniture and display work, dents under aggressive jaws and burns through under careless parameters, so clamping pressure control and tested thin-wall settings matter more than headline capacity. Cosmetic sections, polished stainless and pre-finished tube, need jaw covers and supports that do not scratch; ask to see a polished part come off the machine, not just mild steel.
Joinery Features: The Real Selling Point
Cut-to-length is the least of what the machine does. The features that change a fabrication business are the ones cut into the tube:
⦿ Tabs and slots: mating features that locate parts against each other, so a frame self-assembles square and the fitter's marking-out disappears.
⦿ Copes and saddles: fish-mouth profiles where one tube meets another, cut to fit instead of ground to fit.
⦿ Holes and arrays: bolt patterns and hardware holes placed by program, replacing the drill press and its layout errors.
⦿ Notches and miters: corner joints cut at angle with the weld gap designed in.
Shops describe the downstream effect the same way: welding time drops because fit-up time drops, and quality rises because the parts can only go together one way. For joints that need full weld preparation on the tube ends, the step up is the 3D трубный лазерный станок для резки фасок, which adds angled bevel cutting to the same rotating workflow.
Weld-ready edges and what comes after the cut
Tube parts usually head straight to welding, and the laser's narrow kerf leaves edges that weld without grinding on common wall thicknesses. Pierce points and dross behave as they do on sheet: tuned parameters keep the inside of the tube clean, which matters on sections that carry fluid or stay visible. For production that cannot tolerate any inside dross, discuss the nozzle and gas setup for your wall thickness during the demonstration rather than after delivery.
Automation: When the Bundle Loader Pays
A manual-load machine keeps an operator at the chuck end: load a bar, run the program, catch the parts, repeat. An automatic bundle loader stacks that work: a rack of bars feeds in one after another, parts drop to a conveyor or bin, and the operator becomes a supervisor of several machines or a welder between loads.
The decision is a volume threshold. A shop cutting a few bars a day gains little; a shop running hundreds of repeat parts gains a shift's labor and the lights-out hours after it. Price the loader against the loaded labor cost it replaces, and note that it also steadies quality, because bars feed with the same orientation and pace every time.
Who Buys Tube Lasers, and Which Configuration
⦿ Furniture and display frames: light sections, high part counts, tabs and slots everywhere; a 2 or 3 chuck machine with a loader earns fast.
⦿ Fitness equipment and seating: curved and oval sections with cosmetic surfaces; support quality and scratch-free clamping matter.
⦿ Railings, gates, and fencing: mixed profiles and miters; a flexible manual-load machine covers the variety.
⦿ Machine frames and skids: heavier square sections and bolt arrays; capacity and wall thickness set the spec.
⦿ Contract tube cutting: the service business case, where a loader and near-zero remnant design are the margin.
Finished examples across these industries are collected in the laser cutting machine project gallery, and they are a faster education in what tabs, copes, and arrays look like on real parts than any specification page.
Software carries half the value
The joinery library lives in software, so evaluate it as seriously as the hardware. Good tube software imports 3D assemblies and unwraps each tube's features automatically, places tabs and copes from a menu, and nests parts along bars to squeeze the remnant. Weak software leaves the programmer drawing every notch by hand, which quietly gives back the labor the machine saved. Ask the demonstration to start from your own frame model, not the supplier's sample file.
The Labor Math of Replacing 3 Stations
Take an illustrative frame of forty tubes. Traditionally: forty saw cuts with handling between them, marking out, sixty drilled holes, a dozen milled notches, and fit-up persuasion at the welding table, call it a long day across 3 machines and 2 people. On a tube laser, the same forty parts run from 3 bars in under an hour, arrive deburred of layout error by definition, and lock together for welding.
The saved hours are only half the account. The saw, drill, and mill stations shrink to backup roles, their floor space returns, and the schedule risk of 3 queues becomes one queue. Shops that quote frames weekly find the machine's payback resembles the sheet laser's a decade ago: the 1st mover in a region wins work on lead time until the neighbors catch up. Configurations across capacities and chuck counts are compared on the волоконный лазерный труборез page, alongside the wider fiber laser cutting machine range.
Контрольный список покупателя
✔ List your sections: largest and smallest diameter, heaviest wall, and longest part, with clamping headroom.
✔ Choose chuck count by part length, wall delicacy, and how much remnant yield is worth to you.
✔ Confirm the joinery library: tabs, slots, copes, and miters programmed in the software, not promised in the brochure.
✔ Decide the loader by daily bar count, and leave space for it even if it comes later.
✔ Cut your own frame kit at demonstration, and weld it; the fit-up tells the truth.
Replace the Saw, Drill and Mill with One Program
Compare chuck configurations, capacities, and bundle loaders on the волоконно-лазерная машина для резки труб, and get a free quote matched to your sections, wall thicknesses, and part volumes.